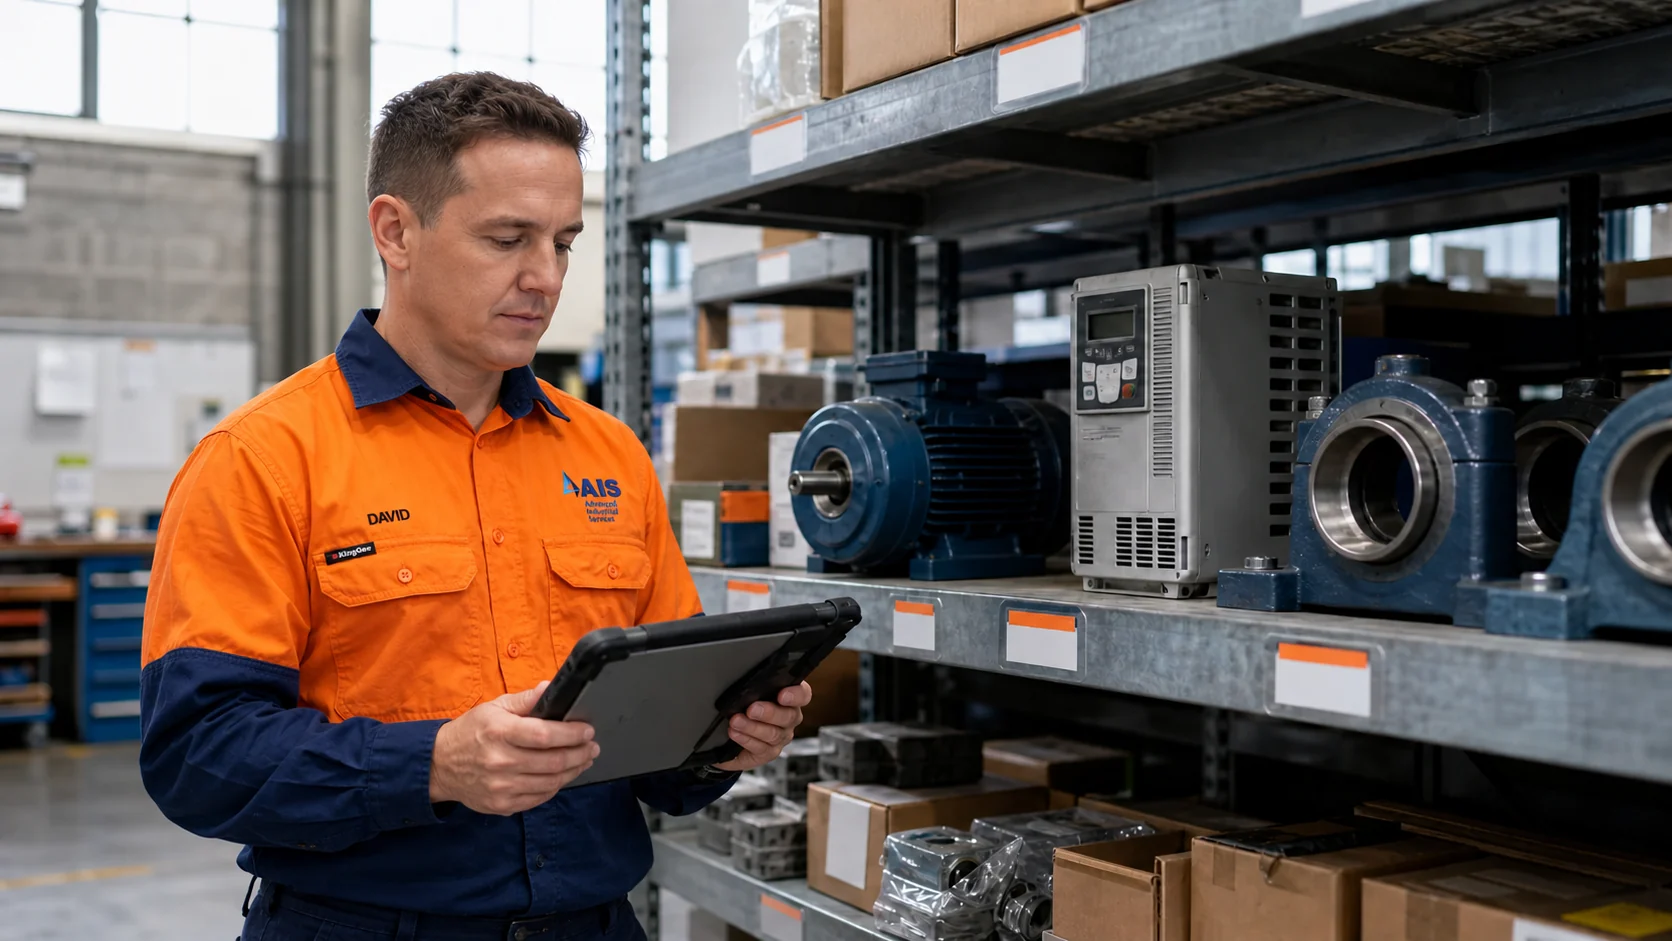
A critical-spares list can grow until almost every component appears essential. That ties up capital without guaranteeing recovery. The useful question is not whether a part could fail. It is whether the site can restore the required function within an acceptable time if that particular part is unavailable.
01 / 03
Rank the consequence of being without the part
Start with the plant function and the consequence of losing it. Consider production, safety, quality, environmental control and whether another line or operating mode can carry the duty. The same motor can be critical in one location and routine in another.
Use consequence to define how long the site can reasonably wait. That recovery requirement becomes the test for each sourcing or repair option.
02 / 03
Map the whole recovery chain
Supplier lead time is only one part of recovery. Check whether the spare needs machining, programming, configuration, special lifting, a shutdown or another trade before it can operate. A component on the shelf is not a ready spare if the site lacks the data or equipment needed to install it.
- 01Confirmed manufacturer and part identity
- 02Realistic supplier or repair lead time
- 03Storage-life and preservation requirements
- 04Required software, parameters, drawings or adaptors
- 05Installation, testing and recommissioning time
03 / 03
Keep the register connected to plant changes
Review critical spares when equipment is modified, a supplier announces obsolescence or the site uses the stocked item. Record compatible alternatives and minimum configuration data rather than relying on one person’s memory.
Inspect stored equipment at a frequency appropriate to the component and environment. Corrosion, flat batteries, degraded seals and uncontrolled firmware can turn an expensive spare into false assurance.
The objective is a credible recovery path—not the largest possible inventory.
The practical takeaway